
 +91 123 456 789
 support@metzix.com
Bucket Elevator
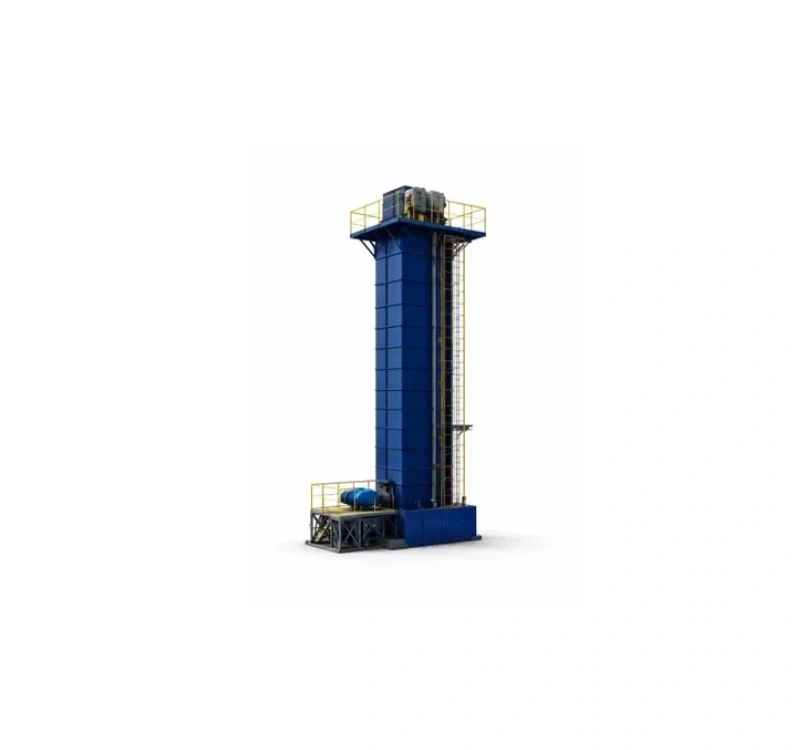
Bucket elevators are engineered for efficient vertical lifting of bulk materials. With a compact design and high lifting capacity, they are ideal for transporting materials to elevated processing stages while maintaining low energy usage.
Engineering Overview
Metzix Continuous and Centrifugal Bucket Elevators provide reliable, space-efficient vertical lifting of free-flowing and sluggish bulk materials to processing heights over 60 meters. Featuring heavy-duty self-supporting steel casings, high-tensile multi-ply rubber belts or forged round-link chains, and reinforced polymer or steel buckets, Metzix elevators minimize material degradation while preventing spillage. Integrated backstops, alignment sensors, and explosion-venting panels ensure safe operations.
Key Features & Engineering Advantages
Performance & Economic Benefits
Minimal horizontal footprint utilizing vertical plant space efficiently
High lift heights exceeding 60 meters with continuous dependable throughput
Completely enclosed dust-tight casing eliminates environmental fugitive dust emissions
Low power consumption per ton lifted compared to pneumatic vertical transport
Technical Specifications
Engineered Standards| Design Parameter / Specification | Technical Standard / Value |
|---|---|
| Lifting Height | Up to 65 meters |
| Throughput Capacity | 10 to 1,200 TPH |
| Traction Element | High-strength Rubber Belt or Case-hardened Alloy Chain |
| Bucket MOC | Hardox, SS304, Cast Iron, Nylon, Polyurethane |
| Safety System | ATEX explosion vent panels, motion and alignment sensors |